A cow dung organic fertilizer pelletizer machine is often sold as a solution. The brochure shows a neat line of equipment, a stream of uniform pellets, and a happy operator. What the brochure does not show is the moisture test that failed, the die that clogged on the first day, or the pile of wet manure that sat waiting for a dryer that was never sized correctly.
The gap between a working pellet line and a failed one is rarely about the machine itself. It is about the material, the preparation, and the realistic expectations of the people running it. Cow dung is not a uniform feedstock. It changes with diet, bedding, season, and storage. A pelletizer that works well with one batch may struggle with the next. Understanding why that happens is more useful than comparing motor power or die diameter.
This article is for buyers, farm managers, and project planners who want to know what actually determines whether a cow dung organic fertilizer pelletizer will perform. It is not a buyer’s guide in the traditional sense. It is a guide to the questions that matter before the machine arrives.
Why Cow Dung Is Not an Ideal Pelletizing Material
Most pelletizing equipment was originally developed for materials like wood sawdust, straw, or feed grains. These materials have relatively consistent moisture, particle size, and binding characteristics. Cow dung is different.
Fresh cow dung contains 75% to 85% moisture. It is biologically active, meaning it continues to decompose and generate heat. It contains fibrous undigested plant material, but also fine particles and soluble nutrients. When it dries, it can become hard and abrasive. When it is wet, it is slippery and prone to clogging.
These characteristics create three main challenges for pelletizing:
Moisture variability. Cow dung moisture changes with weather, feed, and storage. A pile that is 70% moisture on Monday can be 80% on Wednesday after a rain. Pellet mills require a narrow moisture range to operate consistently. Without moisture control, the machine will either clog or produce weak pellets.
Particle inconsistency. Cow dung contains a mix of long fibers, fine particles, and occasional stones or grit. Long fibers can wrap around rollers and shafts. Stones can damage dies. Fine particles can cause blockages. A uniform grind is necessary, but achieving it requires a grinding step that many small operations try to skip.
Biological activity. Fresh manure continues to decompose. If it is pelletized before it is stabilized, the pellets can heat up in storage, develop mold, or lose structural integrity. Composting or drying is not just about moisture reduction. It is also about stabilizing the material so that the final pellet behaves predictably.
These challenges do not mean cow dung cannot be pelletized. They mean that the pelletizer is only one part of a system that must be designed around the material.
The Three Pre-Pelletizing Steps That Decide Everything
Experienced operators will tell you that the pellet mill is the least problematic part of the line. The problems almost always come from upstream. There are three steps that matter more than any machine specification.
1. Moisture Control
The target moisture content for pelletizing cow dung is typically between 12% and 18%. Above 20%, the material becomes difficult to compress and may clog the die. Below 10%, the pellets become brittle and generate excessive fines.
Composting is the most common method for reducing moisture. A properly managed compost pile reaches temperatures of 55°C to 65°C, which drives off water and breaks down volatile compounds. Turning the pile regularly ensures that all material is exposed to the heat. The result is a drier, more stable material that is easier to pelletize.
Mechanical drying can accelerate the process, but it adds capital and energy cost. For small operations, passive composting may be sufficient. For larger operations, a rotary dryer integrated into the line is often necessary to handle continuous production. The decision depends on climate, available space, and production volume.
2. Grinding and Screening
Cow dung compost that has not been ground can contain clumps, fibrous strands, and foreign objects. These cause inconsistent pellet formation and accelerated die wear. A hammer mill or similar grinder is usually required to reduce the material to a consistent particle size.
Screening after grinding removes oversized particles and stones. The goal is a material with a narrow particle size distribution. Large particles create weak points in the pellet. Fine particles can cause die blockage. The ideal grind depends on the die design and the target pellet diameter, but consistency is more important than fineness.
3. Binders and Additives
Cow dung compost often pellets well on its own, especially if it contains some bedding material. But in some cases, a binder improves durability and reduces fines. Common binders include clay minerals, starch, or biochar. Biochar has the added benefit of incorporating carbon into the fertilizer product.
The decision to use a binder should be based on pellet quality requirements and market expectations. Many operations run without binders and achieve acceptable durability. Adding a binder increases cost and complexity, so it should be justified by a specific need, not by a default assumption.
Flat Die vs. Ring Die: Which Pelletizer Fits Your Operation?
Cow dung organic fertilizer pelletizer machines come in two main configurations: flat die and ring die. The choice is not about which is better in absolute terms. It is about matching the machine to the material, the throughput, and the operating pattern.
Flat die pelletizers are common in small to medium operations. They are simpler in design, easier to maintain, and generally less expensive. They work well when the material is relatively dry and the production schedule is not continuous. For a farm that processes a few hundred kilograms to a couple of tonnes per hour, a flat die machine can be a practical choice.
Ring die pelletizers are built for higher capacities and continuous duty. They are more complex, require more careful maintenance, and cost more. But they can handle larger volumes without overheating or excessive wear. For operations that need to run multiple shifts or process several tonnes per hour, a ring die system is usually the better fit.
The choice should be driven by the production schedule, not by a desire to buy the biggest machine available. A small farm that runs a flat die mill for four hours a day may produce the same annual tonnage as a larger farm running a ring die mill for one hour a day. The difference is in labor, maintenance, and how the machine fits into the daily routine.
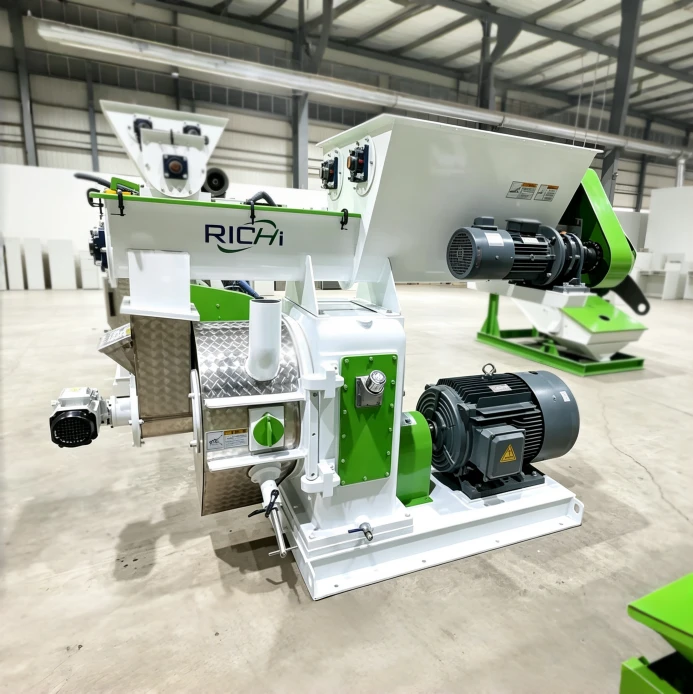
It is also worth considering the full line, not just the pellet mill. A cow dung organic fertilizer pelletizer for farm production is only one component. A complete line may include a compost turner, a grinder, a mixer, a dryer, a cooler, a screener, and a bagging machine. Skipping any of these steps can compromise pellet quality or make the operation uneconomical.
Capacity Planning: Do Not Size for the Best Week of the Year
One of the most common mistakes in pellet project planning is sizing the machine for peak production rather than average production. A farm that produces 10 tonnes of manure per day during the dry season may produce 15 tonnes during the wet season. If the pelletizer is sized for 15 tonnes, it will be underutilized for most of the year.
A more practical approach is to size for the average available feedstock and use a stockpile or custom processing during peak periods. This reduces capital cost and improves utilization. It also avoids the trap of buying a large machine that runs at low capacity, which raises the cost per tonne.
The available feedstock is not the same as total manure production. Some manure is already spread on land. Some is mixed with bedding and used for compost. Some is lost to storage and handling. The material that actually reaches the pellet line is the fraction that is excess, problematic, or specifically designated for processing.
Before selecting a machine, it helps to answer a few practical questions:
- How much manure is currently causing a storage or disposal problem?
- How much is being hauled away at a cost?
- How much is available during the wet season, when drying is difficult?
- How much time and labor can be dedicated to pellet production each week?
The answers define the real feedstock volume. A farm that produces 10 tonnes of manure per day but only has 2 tonnes available for pelletizing does not need a 10-tonne-per-hour machine. It needs a system that can process 2 tonnes per day efficiently and reliably.
Pellet Quality: What Buyers Actually Notice
If the pellets are used on the farm, quality requirements are less demanding. The pellets need to flow through a spreader and break down in the field. Durability and uniformity matter, but they do not need to meet retail standards.
If the pellets are sold, quality becomes a commercial issue. Buyers of organic fertilizer expect consistent pellet size, low moisture, and good durability. A bag of pellets that contains excessive fines or broken pieces looks unprofessional and may not spread evenly.
The key quality parameters are:
- Durability: Pellets should survive handling, bagging, and transport without excessive breakage.
- Uniformity: Pellet diameter and length should be consistent.
- Moisture: Pellets should be dry enough to prevent mold growth during storage, typically below 15%.
- Appearance: Color and surface texture should be uniform.
- Nutrient content: The nutrient profile should be documented and consistent.
These parameters are not achieved by the pellet mill alone. They are the result of the entire process, from feedstock selection to drying and cooling. A well-designed line with proper moisture control and grinding will produce better pellets than a poorly designed line with a high-end pellet mill.
Operating Costs: Where the Money Actually Goes
The purchase price of the pelletizer is only one part of the total cost. A realistic budget must account for the entire production chain, from material handling to final packaging.
Capital cost. A complete cow dung pellet line can range from tens of thousands of dollars for a small, manually operated setup to several hundred thousand dollars for a high-capacity, automated facility. The pellet mill itself may represent only 20% to 40% of the total capital investment. Dryers, grinders, mixers, coolers, screeners, and bagging equipment add significantly to the total.
Energy cost. Pelletizing is energy-intensive. The pellet mill draws substantial power to compress material through the die. Drying, if mechanical, adds thermal energy. Conveying, cooling, and screening add electrical load. Energy cost per tonne varies with material moisture, pellet diameter, and machine efficiency. In regions with high electricity or fuel prices, energy can be the largest operating cost.
Labor. A pellet line is not unattended. It requires operators to feed material, monitor moisture, change dies, perform maintenance, and manage bagging. The labor requirement depends on the level of automation. A fully automated line may need one or two operators per shift. A manual line may need three or four.
Maintenance and wear parts. The die and rollers are consumables. Their lifespan depends on the abrasiveness of the material, moisture consistency, and operating practices. Cow dung compost that contains sand or grit will wear dies faster than clean compost. Budgeting for regular die replacement is part of normal operating cost, not an unexpected expense.
Feedstock cost. If the manure is already being handled as part of farm operations, the feedstock cost is essentially the cost of moving it to the pellet line. If manure must be purchased or transported from another farm, the economics change. Pelletizing only makes sense if the input material is available at low cost and the output product can be sold at a price that covers processing.
The break-even point is different for every farm. A farm that currently pays for manure hauling and spreading has a different starting point than a farm that spreads its own manure on its own land. A farm that can sell bagged organic fertilizer at a premium has a different revenue potential than a farm that uses pellets only for its own fields.
Common Mistakes in Cow Dung Pellet Projects
Several mistakes appear again and again in farm-scale pellet projects. Avoiding them can save significant time and money.
Sizing the machine for peak production rather than average production. A machine that can handle the busiest week of the year will be underutilized for the rest of the year. It is often better to size for average production and use a stockpile or custom processing during peak periods.
Underestimating the importance of drying. Moisture is the single most common cause of pelletizing problems. If the material is too wet, the pellet mill will clog, the pellets will be weak, and the die will wear quickly. Drying is not a step that can be skipped or improvised.
Ignoring feedstock variability. Cow dung is not a uniform material. Its moisture, fiber content, and particle size vary with diet, bedding, storage, and season. A machine that works well with one batch may struggle with the next. Robust preprocessing and consistent blending help reduce variability.
Choosing a machine without considering maintenance. Pellet mills require regular maintenance. Dies wear out. Rollers need adjustment. Bearings need lubrication. If the farm does not have the technical staff or the spare parts supply to maintain the machine, downtime will increase and performance will decline.
Assuming that pellets will sell themselves. Producing a good pellet is only half the challenge. Finding buyers, meeting their quality expectations, and managing logistics are equally important. Before investing in a pellet line, it is worth researching the local market for organic fertilizer and understanding what price the product can command.
A Practical Decision Framework
For a farm or business considering a cow dung pellet project, the decision can be broken down into a sequence of practical steps.
Step 1: Quantify available feedstock. Determine how much cow dung is available for pelletizing on a daily, weekly, and seasonal basis. Account for existing uses and labor constraints.
Step 2: Define the product. Decide whether the pellets will be used on the farm, sold in bulk, or sold in bags. This determines the required quality and the necessary processing steps.
Step 3: Choose the process. Decide between composting, mechanical drying, or a combination. Determine whether grinding and mixing are needed. Select the pellet mill type and size based on feedstock and product requirements.
Step 4: Estimate the full cost. Calculate capital cost, energy cost, labor cost, maintenance cost, and feedstock cost. Compare the total cost per tonne with the expected value of the product.
Step 5: Plan for operation and maintenance. Identify who will run the line, how they will be trained, and how spare parts will be sourced. A pellet line is a production asset, not a piece of equipment that can be ignored between uses.
Step 6: Start at a manageable scale. It is usually better to start with a smaller line and expand later than to invest in a large line that cannot be fully utilized. A modest start allows the farm to learn the process, build market relationships, and refine operations before committing to a larger investment.
For buyers who want to see how different equipment options fit together—from pellet mills to complete organic fertilizer production lines—it can be helpful to review the range of solutions available from experienced manufacturers. Companies like Richi Pelletizer that serve multiple scales and material types often provide practical guidance on line configuration, not just machine specifications.
The Bottom Line
A cow dung organic fertilizer pelletizer machine is not a standalone solution. It is the center of a production system that includes material collection, preprocessing, pelletizing, cooling, screening, and packaging. The success of the project depends less on the machine itself and more on how well the entire system is matched to the farm’s actual material flow, labor availability, and market situation.
The farms that get it right tend to be the ones that start with a clear understanding of their feedstock, choose equipment that fits their realistic production scale, and commit to the preprocessing steps that make good pellets possible. They do not buy a machine because a neighbor did. They buy a system because they have a material problem to solve and a product to sell.
That is the difference between a pellet line that runs for a few weeks and one that becomes a permanent part of the farm’s operation.